Tel/WhatsApp:+86 18011919834
E-mail: chloe.x@fybagcustom.com

Tel/WhatsApp:+86 18011919834
E-mail: chloe.x@fybagcustom.com

Who this guide is for: product developers, sourcing managers, backpack and travel brand owners, Amazon sellers and promotional buyers who need to choose between nylon and polyester for a custom bag line.
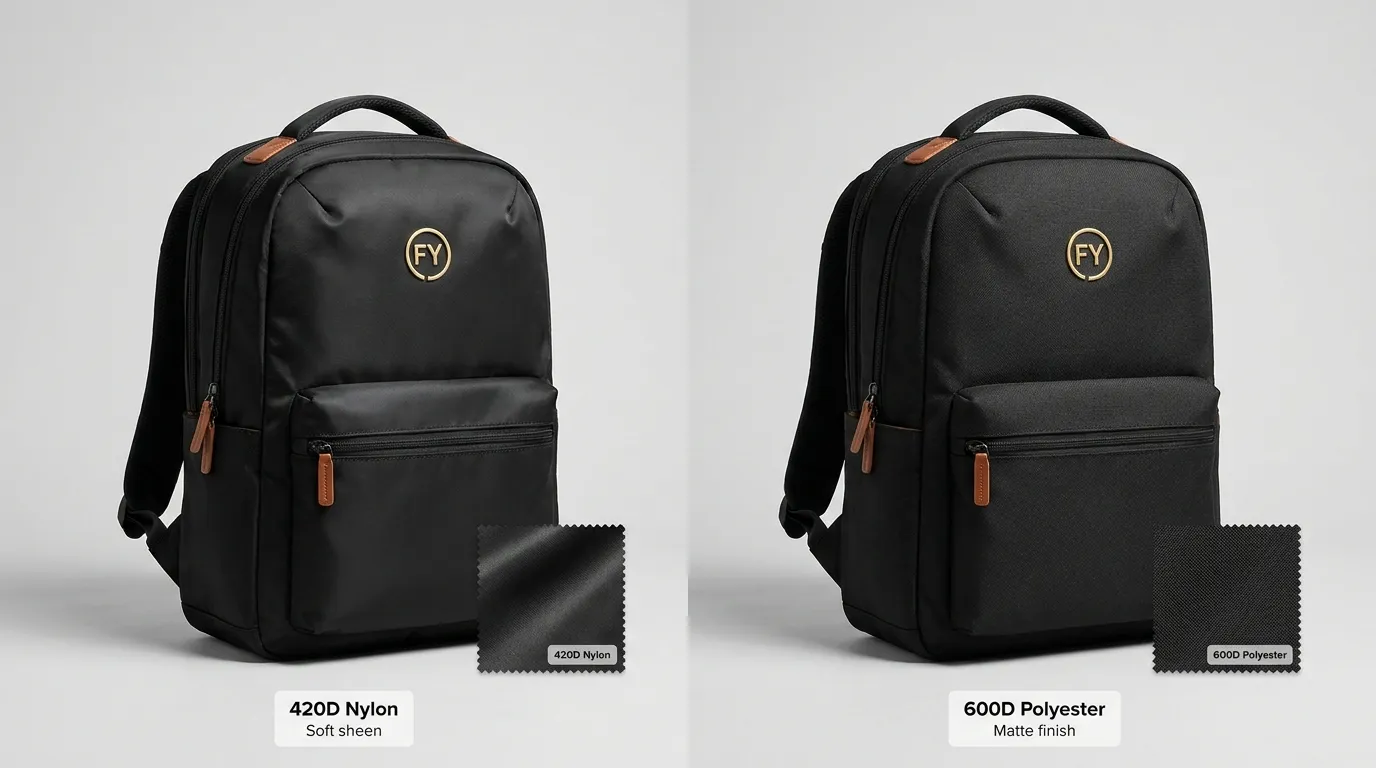
The nylon vs polyester fabric for bags question comes up in nearly every backpack, travel bag and pouch quote. On a spec sheet both fabrics can read “420D” or “600D”, and a sewing line handles them the same way. In use they part ways. Nylon gives more strength and a softer hand at the same weight. Polyester holds color, shrugs off sunlight and costs less.
Quick answer: Nylon is stronger, more abrasion-resistant and softer than polyester of the same denier, so it suits premium backpacks, travel bags and lightweight handbags. Polyester costs less, resists UV fading and stretching better, absorbs less water and accepts sublimation printing, so it suits promotional bags, school bags, cooler shells and printed designs.
Both are synthetic thermoplastic fibers made from petrochemicals or recycled feedstock. The chemistry differs, and that difference explains the performance gaps buyers notice in use.
Nylon is a polyamide. Bag fabrics use two main types. Nylon 6 is the more common and lower-cost grade. Nylon 6,6 has a tighter molecular structure, a higher melting point (roughly 260°C against roughly 220°C for nylon 6) and better abrasion resistance. Most branded high-tenacity bag fabrics use nylon 6,6.
Polyester in bags almost always means PET, the same polymer used in drink bottles. That shared chemistry explains the wide supply of recycled polyester (rPET).
The key property differences:
The table summarizes the trade-offs at a similar denier and construction. Mills vary, so treat it as a starting point for your fabric brief.
| Property | Nylon | Polyester | What it means for your bag |
|---|---|---|---|
| Tear and tensile strength | Higher | Good | Nylon allows a lighter fabric for the same strength |
| Abrasion resistance | Higher | Good | Nylon suits bag bases and travel use |
| Stretch | More | Less | Polyester keeps shape and print panels flat |
| Moisture absorption | Roughly 4% | Under 1% | Polyester dries faster and sags less |
| UV resistance | Fair | Good | Polyester suits beach and outdoor bags |
| Hand feel | Soft, smooth, slight sheen | Crisper; varies by finish | Nylon reads more premium in handbags |
| Printing | Screen, heat transfer, embroidery | Adds sublimation | Polyester wins for all-over prints |
| Recycled option | Recycled nylon, tighter supply | rPET, wide supply | rPET is easier to source at volume |
| Relative fabric cost | Higher | Lower | Polyester fits tight cost targets |
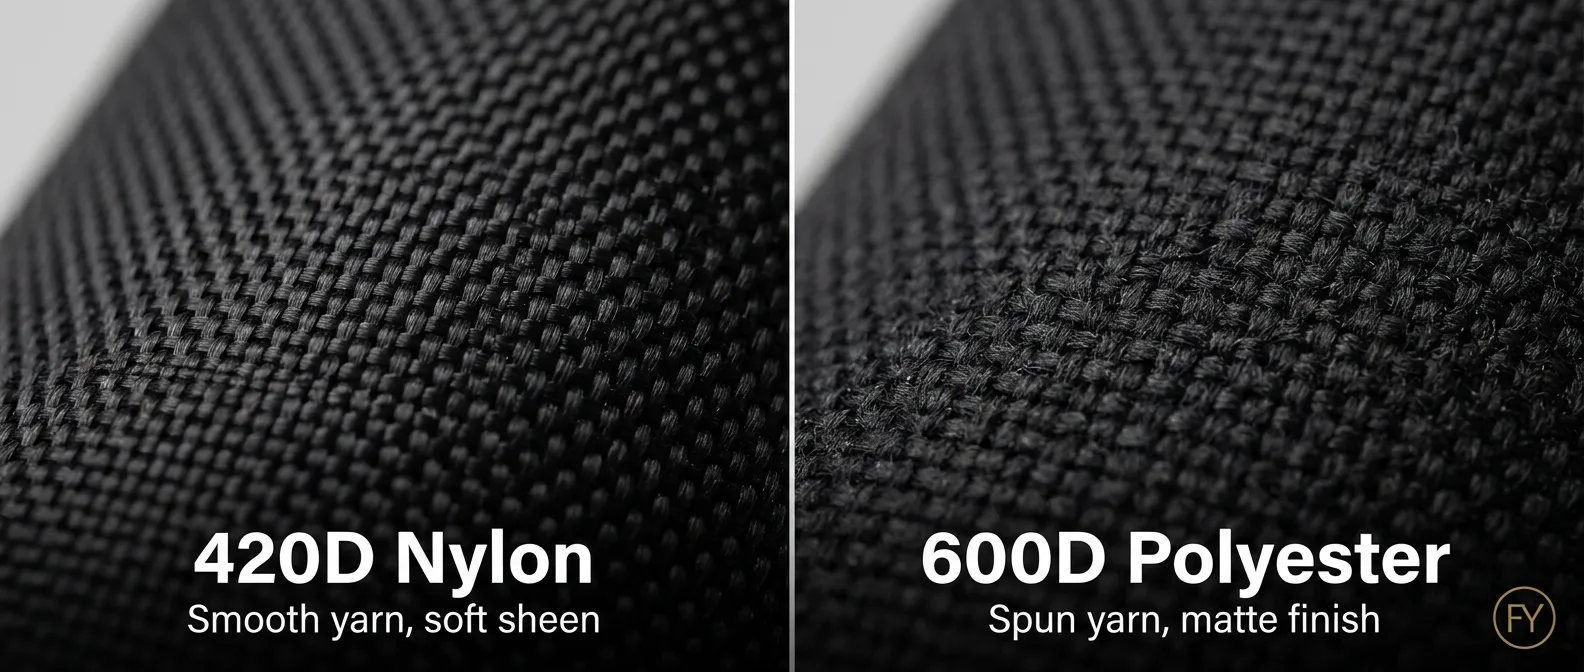
Denier is the mass in grams of 9,000 meters of a single yarn. A higher number means a thicker yarn. It does not, on its own, tell you how strong the finished fabric is. Weave density, yarn type (standard or high-tenacity, flat or air-textured) and coating all change the result. A well-built 420D high-tenacity nylon can outperform a loosely woven 600D polyester in tear testing.
| Denier range | Where you see it | Usual fiber | Character |
|---|---|---|---|
| 70D–210D | Linings, packable bags, ripstop shells | Nylon or polyester | Light and thin |
| 300D–420D | Backpacks, crossbody bags, cosmetic pouches | Both; 420D nylon common in packs | Medium weight |
| 600D | Promotional backpacks, school bags, cooler shells | Mostly polyester | Stiff once backed with PU or PVC |
| 840D–1050D | Premium backpacks, luggage panels | Mostly high-tenacity nylon | Heavy and tough |
| 1680D ballistic | Luggage, tool bags, reinforced bases | Nylon or polyester | Heaviest; basket weave |
Ripstop adds a grid of thicker yarns every few millimeters, which stops small tears from running. It suits lightweight ripstop nylon handbags and packable travel bags where you want low weight without fragility.
Watch for fiber substitution. Some suppliers quote “nylon” and deliver polyester, because the two look alike once coated. A burn test gives a rough first check in the sampling room: nylon melts with a celery-like smell, while polyester gives a sweetish smell and darker smoke. For bulk, ask for a fiber content test from an independent lab under a method such as AATCC 20/20A or ISO 1833.
Uncoated nylon and polyester both let water through the weave. Most bag fabrics carry a back coating or lamination, and that layer often matters more for water resistance than the fiber choice. If you need a fully waterproof bag, plan sealed or welded seams and water-resistant zippers as well, because coated fabric alone only makes a bag water-resistant.
| Coating or finish | What it does | Water resistance | Hand and weight | Watch for |
|---|---|---|---|---|
| PU coating (1–3 passes) | Seals the back of the weave | Moderate; rises with passes | Light, flexible | Can hydrolyze and peel after years in heat and humidity |
| PVC backing | Thick, stiff back layer | High | Heavy, stiff | Plasticizer and phthalate rules, especially for children’s bags |
| TPU lamination | Film bonded to the back | High; allows welded seams | Medium, durable | Higher cost; better aging than many PU coatings |
| DWR finish | Makes the face bead water | Surface only | No change | Specify PFAS-free (C0) chemistry |
| Silicone impregnation | Saturates thin nylon | High | Lightest option | Hard to print, glue or seam-tape |
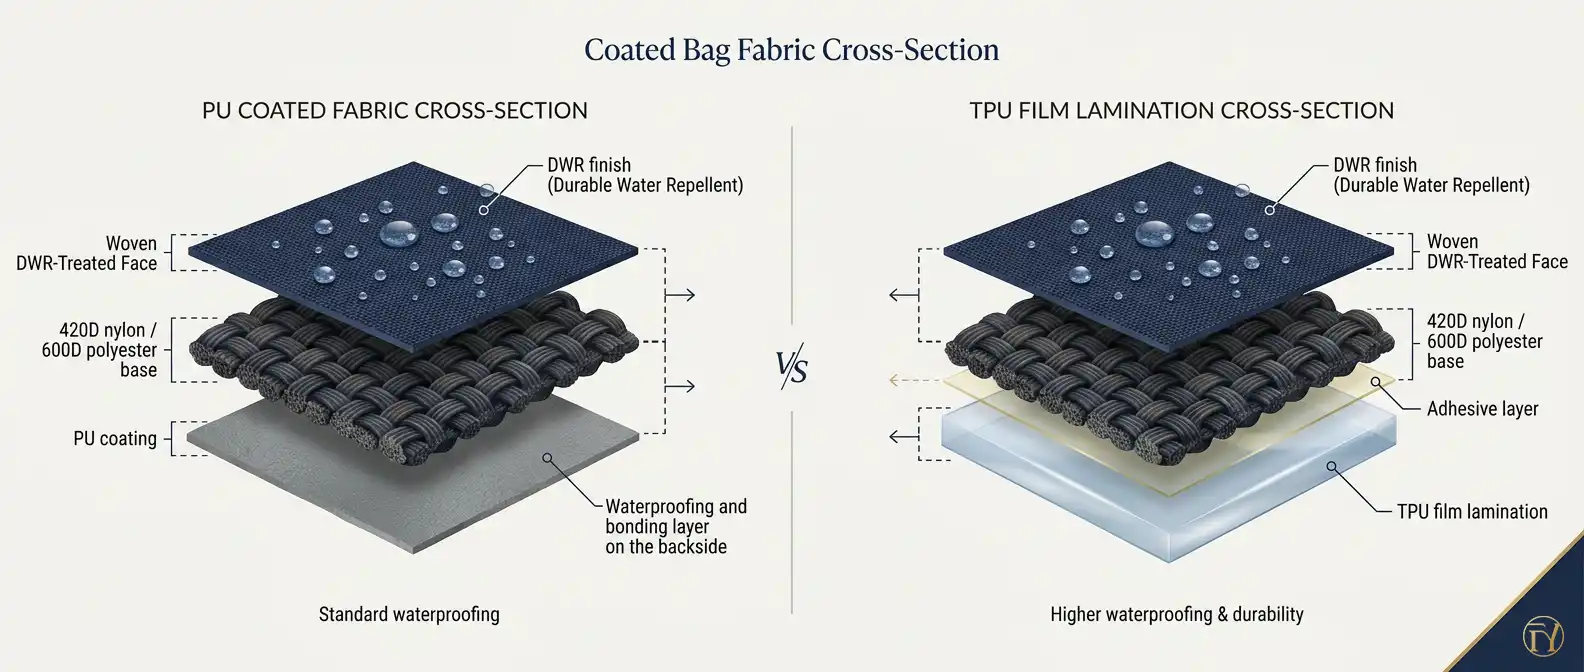
Buyers measure water resistance as hydrostatic head, reported in millimeters under ISO 811 or AATCC 127. Ask your mill for the value on the bulk lot, and ask how it holds after flexing, since coatings crack at fold lines first.
PVC-backed 600D polyester remains common in low-cost backpacks and coolers. It is stiff, heavy and inexpensive. If you sell the bag for children in the United States, CPSIA limits on lead and certain phthalates apply, and the EU’s REACH rules restrict several phthalates across consumer goods. TPU and PU backings avoid most of those questions.
DWR chemistry has shifted too. Several U.S. states now restrict intentionally added PFAS in textile products, and some of those laws name bags and backpacks. Specify PFAS-free DWR in your tech pack and ask the mill to confirm it in writing.
The right fiber depends on the bag’s job. The table gives a sensible default for common categories.
| Bag type | Better default | Why |
|---|---|---|
| Premium travel or commuter backpack | Nylon, 420D–1050D, high-tenacity | Abrasion resistance and strength-to-weight |
| School or promotional backpack | Polyester, 600D | Lower cost, stable color, easy printing |
| Soft nylon handbag or tote | Nylon twill or taffeta | Smooth hand and sheen buyers read as premium |
| Packable or foldable bag | Ripstop nylon or light polyester ripstop | Low weight, tear control |
| Cooler or lunch bag shell | Polyester, 600D | Holds shape, low moisture absorption, prints well |
| Beach or outdoor tote | Polyester or rPET | Better UV resistance |
| Cosmetic pouch or GWP bag | Polyester for cost; nylon for premium | Depends on the price tier |
| All-over printed bag | White polyester | Only polyester takes sublimation |
| Duffle or luggage base | Ballistic nylon or 1680D polyester | Maximum abrasion resistance |
For custom backpacks, many brands mix both: nylon on the base and high-wear panels, polyester on the body or lining to manage cost. The same split works on duffles and travel bags.
Our custom nylon bag page shows the nylon handbag, tote and crossbody formats brands develop most often. The polyester bag page covers the denier range from 210D to 1680D, rPET and sublimated options.
Nylon fabric usually costs more than polyester of a comparable denier and construction. High-tenacity and branded nylons sit higher again. Recycled nylon carries a premium over virgin nylon and comes in a narrower color and denier range. The premium for rPET over virgin polyester has narrowed as supply has grown, and for common deniers it can be small.
| Fabric option | Relative fabric cost | Effect on finished bag cost |
|---|---|---|
| 600D polyester, PU or PVC backed | Low | Baseline |
| rPET 600D | Low to Moderate | Small increase |
| 420D nylon, PU coated | Moderate | Moderate increase |
| 840D–1050D high-tenacity nylon | High | Noticeable increase |
| Branded high-tenacity nylon | Highest | Premium tier |
| Recycled nylon | High | Noticeable increase; supply varies |
| TPU-laminated nylon or polyester | Moderate to High | Increase plus welding labor if seams are sealed |
Keep the fabric premium in proportion. On a structured backpack, labor, zippers, webbing, buckles and padding make up a large share of the unit cost, so switching the body fabric from polyester to nylon raises the total by less than the fabric price gap suggests. On a simple pouch, fabric is a bigger share and the gap shows more.
Color minimums matter as much as fiber. Mills usually hold stock colors in common deniers. A custom shade often needs a dye lot minimum at the mill, which can exceed what a small order uses. Choosing a stock color for the first run, then moving to a custom shade on reorder, is a common way to keep early orders lean.
rPET is the easier recycled fiber to source. Bottle-grade PET waste is plentiful, and mills offer rPET in most common deniers, colors and coatings. Recycled nylon comes from pre-consumer factory waste and from post-consumer sources such as old fishing nets and carpet fiber, and its supply is tighter. Expect fewer stock colors, longer mill lead times and a larger premium.
Both claims need documentation. Ask the mill for a transaction certificate under a chain-of-custody standard such as the Global Recycled Standard (GRS) or the Recycled Claim Standard (RCS) for the lot you buy, and keep it with your order records. Without that paper trail, a “recycled” line on your hang tag is hard to defend.
If a recycled claim matters most for your line, polyester makes it simpler. If nylon performance matters more, recycled nylon works, but plan it into the calendar earlier.
Ask for these before you approve bulk fabric, ideally on the actual production lot:
Mill test reports help, but they often come from an earlier lot. For a first order of a new fabric, an independent test on the bulk lot gives you a record you can rely on.
FYBagCustom is Your Trusted Custom Bag Manufacturer in China, developing nylon and polyester backpacks, handbags, totes, pouches and travel bags for brands, wholesalers and e-commerce sellers through OEM, ODM and private label programs.
FYBagCustom, a custom bag factory in Huadu District, Guangzhou, sources fabric through a network of 200+ verified suppliers, covering standard and high-denier nylon, polyester and rPET with PU, PVC or TPU backings. Behind that sit 15+ years of production, a 5,000 m² facility, 500+ staff and 10+ production lines.
For a fiber decision, the practical step is a side-by-side sample:
Share your target bag, denier and coating needs with our team, and we will suggest fabric options that fit your use case and cost target.
Nylon is better for premium, travel and heavy-use backpacks because it resists abrasion and tearing more at the same weight. Polyester is the better value for school, promotional and everyday backpacks, where stable color and lower cost matter more. Many brands combine them, with nylon on the base and high-wear panels and polyester on the body or lining.
Neither fiber is waterproof on its own. Polyester absorbs less water and dries faster, while nylon absorbs roughly 4% of its weight in moisture. Water resistance comes mainly from the coating or lamination: PU, PVC or TPU. A fully waterproof bag also needs sealed or welded seams and water-resistant zippers, whichever fiber you choose.
Not necessarily. Denier measures yarn thickness, not fabric strength. Weave density, high-tenacity yarns and coatings all change performance, so a 420D high-tenacity nylon can outperform a loosely woven 600D polyester. Compare tensile, tear and abrasion test results on the actual fabric instead of relying on the denier number in a quote.
No. Sublimation dyes bond with polyester fibers and do not fix properly in nylon. For full-color, all-over artwork, use white or pale polyester or rPET. On nylon, use screen printing, heat transfer, embroidery or printed patches. Some mills offer digitally printed nylon fabric before cutting, which is another route for patterned nylon bags.
A burn test in the sampling room gives a quick indication: nylon melts with a celery-like smell, while polyester smells sweetish and gives darker smoke. The test is rough and needs care. For bulk orders, ask for a fiber content test from an independent lab, using a method such as AATCC 20/20A or ISO 1833.
FYBagCustom’s OEM/ODM team helps backpack brands, Amazon sellers and promotional buyers compare nylon, polyester and rPET on the same pattern. Get 5–7 day side-by-side samples, flexible MOQ blended across colors, and decoration from embroidery to sublimation.
Start Your Custom Bag Project →